How Is Injection Moulding Used to Make Plastic Products?
Bottle caps, phone cases and car parts are made by forcing molten plastic into a steel mould under high pressure. Here is how each injection moulding cycle works, and why parts sometimes go wrong.
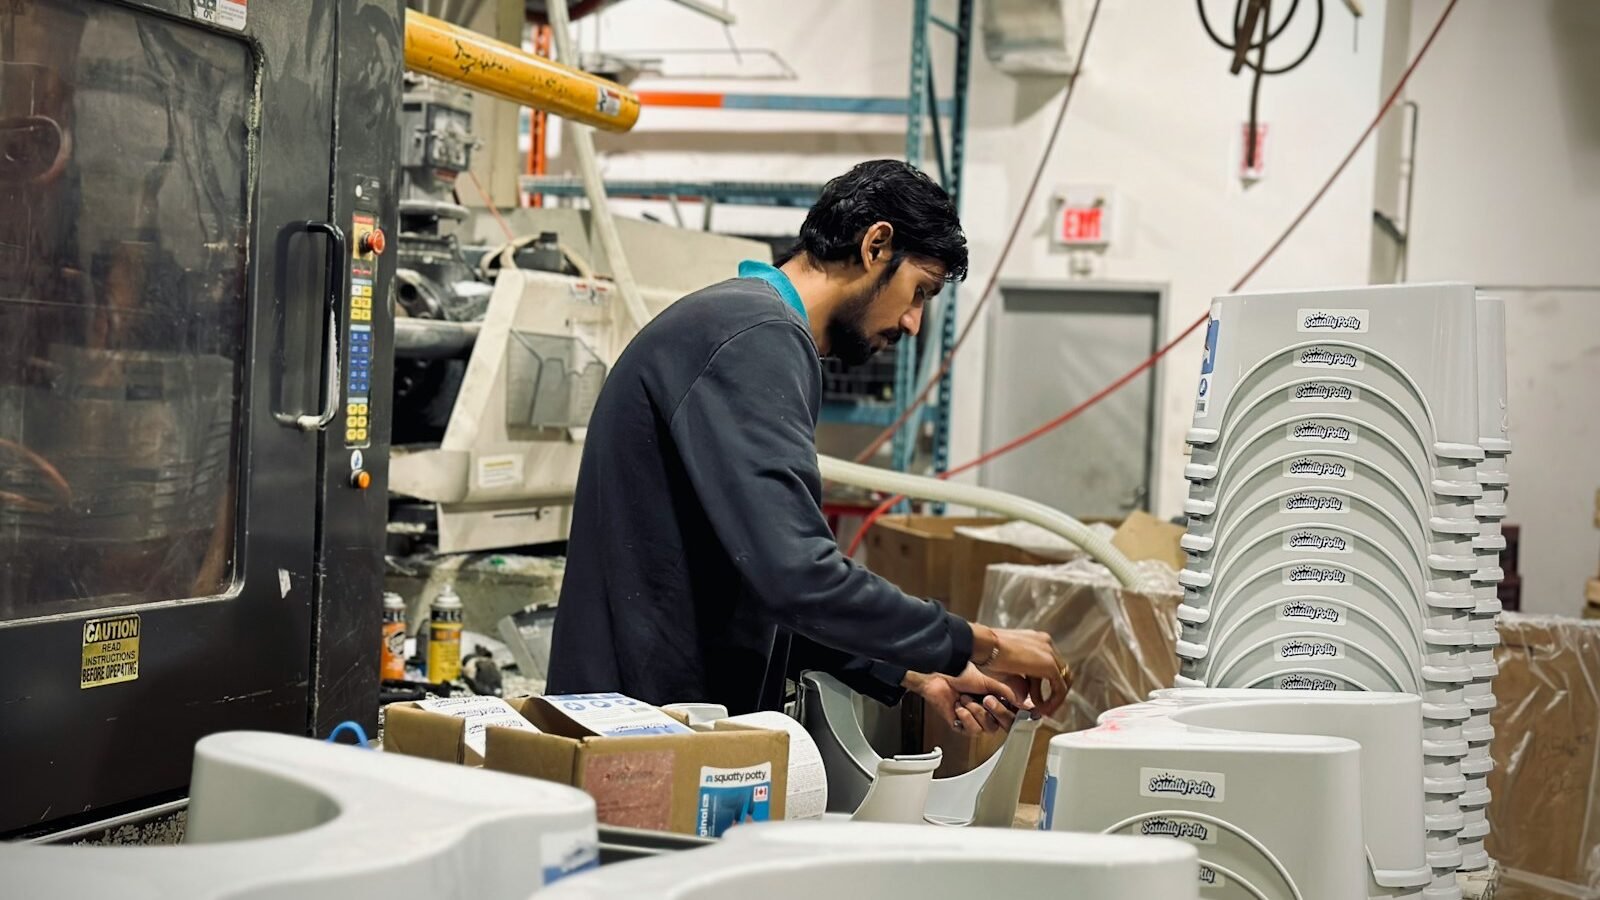
Look around almost any room and you will find injection-moulded plastic: bottle caps, remote controls, toothbrush handles, power sockets, toy bricks, car dashboards. Many of these parts are produced in cycles lasting well under a minute each, with every part almost identical to the last.
The idea is simple: melt plastic, squirt it into a shaped cavity, let it cool, and pop the part out. Doing that quickly, repeatably and without defects is where the engineering lies, and it explains the small details you can spot on almost every plastic part.
The short answer
- Plastic pellets are melted in a heated barrel by a rotating screw, then injected under high pressure into a closed steel mould.
- Extra plastic is packed in while the part cools, to make up for the plastic shrinking as it solidifies.
- Cooling usually takes up the largest share of each cycle. The mould is kept cool by water flowing through channels inside it.
- The mould opens and ejector pins push the part out. Tapered walls (draft angles) and even wall thickness help prevent defects.
The basic principle: shape the plastic while it is liquid
Thermoplastics, the most common plastics used in injection moulding, soften when heated and harden again when cooled. That makes them ideal for a process that melts them, forces them into a precise shape, and freezes that shape in place.
An injection moulding machine has two main parts:
- The injection unit melts the plastic and pushes it into the mould.
- The clamping unit holds the two halves of the mould tightly together against the injection pressure, then opens them to release the part.
The mould itself is usually machined from steel or aluminium. It contains the cavity, which is a negative of the part, plus channels for the plastic to flow in and for cooling water to circulate.
How it works, step by step
- Feeding and melting. Plastic pellets are fed from a hopper into a heated barrel. A rotating screw carries them forward, and heat from the barrel walls plus friction from shearing melts them into a uniform liquid.
- Clamping. The clamping unit closes the two halves of the mould and holds them shut with enough force to resist the pressure of the incoming plastic.
- Injection. The screw moves forward like a plunger, forcing the molten plastic through a nozzle and into the mould, along channels called the sprue and runners, through a small opening called the gate, and into the cavity.
- Packing and holding. Once the cavity is full, the machine switches from controlling the injection speed to controlling pressure. It keeps pushing extra plastic in to compensate for shrinkage as the material starts to cool.
- Cooling. The plastic cools and solidifies against the mould walls, which are kept at a controlled temperature by water or another coolant circulating through channels. Meanwhile, the screw draws back and melts plastic for the next shot.
- Ejection. When the part is solid enough, the mould opens and ejector pins push it out. The mould closes again and the next cycle begins.
- Finishing. Runners and sprues are trimmed off and often reground for recycling, where the material allows.
The science behind it
Shrinkage and the packing stage
Plastics take up more space when hot and molten than when cold and solid. As a part cools in the mould, it shrinks. If nothing were done, thick areas would pull inward and leave dents or internal voids.
The packing stage counters this. Holding pressure forces more molten plastic into the cavity as the material shrinks. The moment the machine switches from filling to packing is one of the most critical settings in the whole process. Too little packing leaves sink marks; too much can make parts stick in the mould or go out of tolerance.
Why cooling dominates
Plastics conduct heat poorly, so heat has to travel slowly from the centre of the part to the cooled mould walls. Cooling time depends on wall thickness, the thermal properties of the plastic and the temperature at which it can safely be ejected. Thicker walls take disproportionately longer to cool, which is one reason designers keep walls as thin and uniform as practical.
Designing parts that mould well
Several features you can see on everyday plastic parts exist because of the process:
| Feature | Why it is there |
|---|---|
| Draft angle | A slight taper on walls parallel to the mould opening direction, often around 1–2°, so the part releases without scuffing or sticking. |
| Uniform wall thickness | Even walls cool evenly. Thick spots shrink more and cause sink marks or warping. |
| Ribs | Thin internal ribs add stiffness without creating thick, slow-cooling sections. |
| Gate mark | A small blemish where the plastic entered the cavity. |
| Ejector pin marks | Small round marks, usually on hidden faces, where pins pushed the part out. |
Real-world applications
- Packaging, especially bottle caps and closures, which need precise threads and are made in enormous numbers.
- Consumer products such as appliance housings, toys and kitchenware.
- Automotive parts, from interior trim to clips and housings.
- Medical devices such as syringes and housings, where repeatability and cleanliness are essential.
- Multi-material parts, where two different plastics are moulded into the same tool, for example a rigid handle with a soft grip.
Common misconceptions
“Injection moulding is cheap for everything”
Each part can be very cheap, but the mould is expensive to design and machine. Injection moulding makes economic sense mainly at high volumes, where the tooling cost is spread across many parts.
“The plastic is simply poured in”
Molten plastic is viscous, so it is forced in under high pressure. The machine controls injection speed, pressure and timing precisely, and those settings strongly affect part quality.
“Defects mean bad material”
Most moulding defects trace back to part design, tooling or process settings rather than the plastic itself, for example uneven walls, poorly placed gates, inadequate venting or incorrect melt temperature.
Limitations and exceptions
- Common defects. Sink marks are depressions caused by uneven cooling and shrinkage, often opposite thick sections. Warping occurs when different areas shrink by different amounts. Short shots are parts that did not fill completely. Knit lines appear where two flow fronts meet.
- Material handling. Some plastics absorb moisture and must be dried before moulding, or defects and loss of strength can result.
- Geometry limits. Undercuts and internal features that would trap the part in the mould need extra moving parts in the tool, adding cost.
- Plastics age. Moulded parts can still degrade over time with heat and sunlight, as described in why plastic products turn yellow.
Frequently asked questions
How long does one injection moulding cycle take?
It varies with the part and material. Industry guides commonly cite cycle times from well under a minute to a couple of minutes, with cooling taking up much of that time.
What is the little nub on many plastic parts?
Often it is the gate vestige, the point where molten plastic entered the cavity, trimmed after moulding.
Can one mould make several parts at once?
Yes. Multi-cavity moulds produce several identical parts per cycle, which is common for small, high-volume items such as caps.
Is injection moulding only for plastics?
Thermoplastics are the main materials, but related processes also inject metals and ceramics mixed with binders, and some rubbers and thermosetting plastics are moulded in similar ways.
For another high-speed process that turns raw material into identical products, see how aluminium cans are made.
References
- Protolabs Network (formerly Hubs). Injection molding machines and how they work.
- Protolabs. An A-to-Z Guide for Injection Moulding Terminology.
- Texas Injection Molding. How Injection Molding Works.
- Omnex. Product Knowledge: Injection Molding (PDF).
- Glow Scotland, Design and Manufacture resources. Injection Moulding (PDF).
- Makerverse. How Injection Moulding Works: Complete Step-by-Step Process.
Header photo: Jay Bhadreshwara on Unsplash.