How Are Aluminium Cans Manufactured?
A drinks can starts as a flat disc of aluminium alloy and is stretched, thinned and shaped in seconds. Here is how cupping, drawing and wall ironing turn sheet metal into a can.
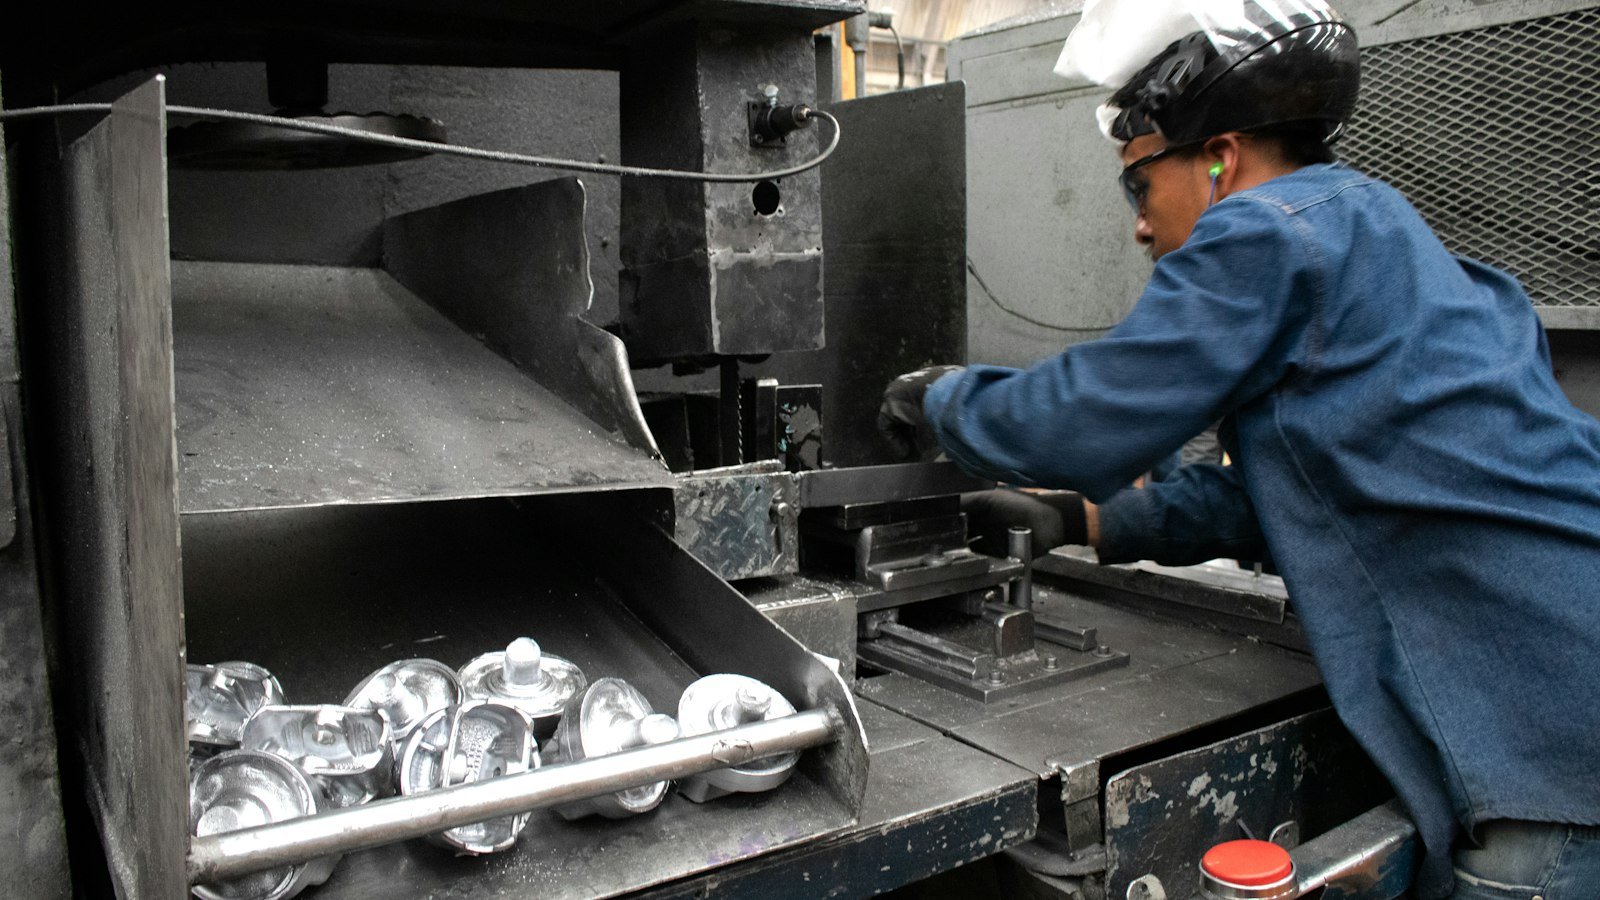
An empty drinks can weighs very little, yet when filled and sealed it can be stacked several layers high on a pallet without collapsing. Its walls are thinner than a sheet of paper in places, and its body is a single seamless piece of metal with no joins down the side. All of that comes from a sequence of forming steps that turns a flat disc of aluminium into a can body in a fraction of a second.
The standard drinks can is called a two-piece can: one piece is the seamless body, including the base, and the other is the lid. The process that makes the body is known as drawing and wall ironing, often abbreviated to DWI or D&I.
The short answer
- Can bodies are made from coils of aluminium alloy sheet, commonly alloy 3104 in a very hard temper, roughly 0.2 to 0.3 mm thick.
- A cupping press punches out discs and forms them into shallow cups.
- A bodymaker redraws each cup to a smaller diameter and pushes it through a series of ironing rings that stretch and thin the walls, forming a tall, thin-walled cylinder with a domed base.
- The body is then trimmed, washed, coated, printed, necked and flanged. The lid is made separately and seamed on after filling.
The basic principle: stretching metal instead of joining it
A can body could in principle be made by rolling a sheet into a tube, welding the seam and attaching a base, as many food cans once were. Drinks cans avoid seams altogether. Instead, a disc of metal is forced through dies in two different ways:
- Drawing pulls the flat metal into a cup or cylinder shape, reducing its diameter without much change in thickness.
- Ironing squeezes the wall of that cylinder between a punch and a ring with a slightly smaller gap than the wall thickness. The metal has to go somewhere, so the wall gets thinner and longer.
Because the base is not ironed, it stays relatively thick, while the walls become extremely thin. The result uses very little metal for its size.
How it is made, step by step
- Uncoiling and lubrication. A coil of aluminium sheet is unwound and coated with a thin film of lubricant to help the metal slide through the tools.
- Cupping. A cupping press cuts circular discs, called blanks, from the sheet and immediately draws each one into a shallow cup. The leftover skeleton of sheet is collected for recycling.
- Redrawing and ironing. Each cup goes to a bodymaker. A punch pushes the cup through a redraw die, which reduces its diameter and makes it taller, then through a series of ironing rings, typically several in a row, each thinning the wall a little more.
- Doming. At the end of the stroke, the base is pressed against a tool that forms the inward dome on the bottom of the can.
- Trimming. The top edge after ironing is uneven, so the can is trimmed to a precise height.
- Washing. Cans are washed to remove lubricant and prepare the surface for coating.
- Decorating and coating. The outside is printed with the brand design, and the inside is sprayed with a thin protective coating that separates the drink from the metal. The coatings are cured in ovens.
- Necking and flanging. In a series of stations, the top of the can is gradually squeezed to a smaller diameter, forming the neck, and its edge is turned outward to form a flange.
- Testing and shipping. Cans are inspected, often including light testing for pinholes, and shipped empty to filling plants.
- Filling and seaming. At the beverage plant, the can is filled and the lid is attached by folding the lid’s edge and the can’s flange together into a tight mechanical seam.
The science behind it
Why alloy 3104?
Pure aluminium is soft. Can bodies are typically made from alloy 3104, an aluminium alloy containing manganese and magnesium, supplied in a fully hardened condition called the H19 temper. It combines low density and good corrosion resistance with high strength, while still being formable enough to survive drawing and heavy ironing. One industry patent describes typical body sheet as 3104-H19 with a thickness between 0.2 and 0.3 mm.
Lids need different properties. They are usually made from a harder, magnesium-rich alloy such as 5182, because the lid has to be stiff enough to resist internal pressure and to form the score line and rivet for the ring-pull.
Work hardening
As aluminium is deformed at room temperature, its internal crystal structure fills with dislocations, which are line defects in the arrangement of atoms. These tangle and make further deformation harder. This is work hardening, and it is why the heavily ironed can wall ends up much stronger than you might expect from its thickness.
The same effect makes the process demanding. Each ironing step pushes the metal closer to its limit, and if the wall is thinned too much, or if there is a flaw in the sheet, it can tear. Engineers use computer simulations of how the alloy flows under large plastic deformation to optimise the tools and reduce such failures.
Why the dome and the neck?
The domed base resists internal pressure better than a flat base of the same thickness, in the same way an arch carries load. Necking reduces the diameter of the opening, so the lid can be smaller. Since the lid is made of thicker, stronger alloy, a smaller lid saves metal.
Real-world applications
- Beverages. Soft drinks, beer, sparkling water and energy drinks are the main use of DWI aluminium cans.
- Bottle-shaped cans. Some aluminium bottles are made by the same drawing and ironing route followed by extensive necking to form a narrow, threaded neck.
- Aerosols. Many aerosol cans are made by a different process called impact extrusion, in which a thick slug of softer aluminium is struck so hard that it flows up around a punch.
Common misconceptions
“A can is made of pure aluminium”
Can bodies and lids are aluminium alloys chosen for strength and formability. Pure aluminium would be too soft to make cans this thin.
“The drink touches bare metal”
The inside of a drinks can is coated with a thin protective lining. It stops acidic or carbonated drinks reacting with the aluminium and protects the taste of the contents.
“Cans are made from one sheet rolled into a tube”
Drinks can bodies are seamless. The body, including its base, is drawn and ironed from a single disc.
Limitations and exceptions
- Empty cans are fragile. A filled, sealed can of a carbonated drink gains much of its stiffness from internal pressure. Empty, the thin walls dent easily.
- Defects matter. Because the walls are so thin, small inclusions or scratches in the sheet can cause tears during ironing or pinholes in finished cans, which is why cans are tested before shipping.
- Not all cans are made this way. Many food tins are steel, and some cans are three-piece designs with a welded side seam.
Frequently asked questions
How thin is the wall of a drinks can?
The starting sheet is only a few tenths of a millimetre thick, and the ironed walls are thinner still. The base and the top edge remain thicker than the middle of the wall.
Why do cans have a concave bottom?
The inward dome helps the base resist internal pressure without bulging, while using thinner metal than a flat base would need.
When was the two-piece drawn and ironed can introduced?
Published research on the process dates the first drawn and ironed two-piece beverage can manufacturing process to 1963.
Why does the lid use a different alloy from the body?
The body must stretch and thin dramatically, while the lid must be stiff and hold a scored opening and riveted tab. Different alloys suit those different jobs.
For another example of how a manufacturing process creates strength from built-in stresses, see how tempered glass is made.
References
- United States Patent 10,807,140. Optimized drawing and wall ironing process of aluminum containers.
- United States Patent 11,565,534. Method for manufacturing cans for beverage (process line: uncoiler, lubricator, cupping press, bodymaker, trimmer, washer).
- United States Patent 10,675,669. Method for producing a beverage can, a bottle-can or an aerosol can from aluminium alloy.
- A Flow Stress Model of the AA3104-H19 Alloy for the FEM Simulation of the Beverage Can Manufacturing Process under Large Plastic Deformations. Materials (2021), 14(21), 6408.
- AL Circle. A step-by-step guide to aluminium can manufacturing process.
Header photo: Salvador Escalante on Unsplash.